


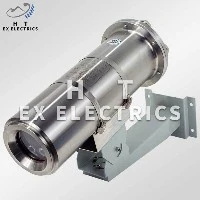
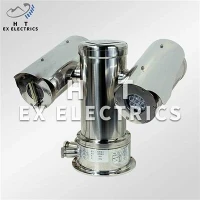

Explosion-Proof Fiber Optic Camera
Your Professional Explosion-Proof Fiber Optic Camera Supplier
Mining operations in hazardous underground environments require video surveillance equipment engineered for safety compliance, optical network integration, and durable performance. HT EX supplies industrial-grade camera solutions designed for coal mine monitoring, covering explosion-proof PTZ units, intrinsically safe cameras, and optical signal transmission systems.
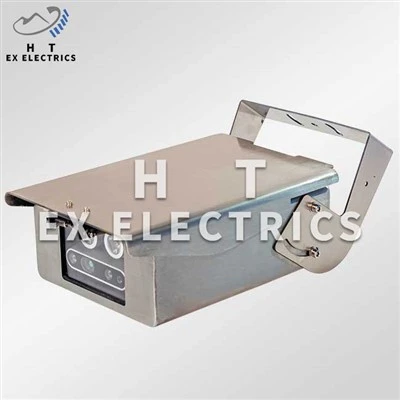
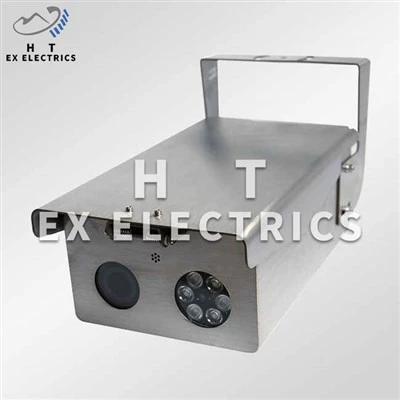

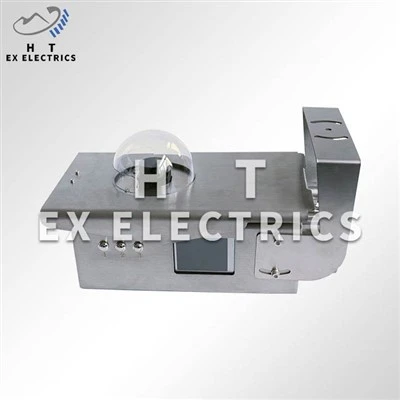
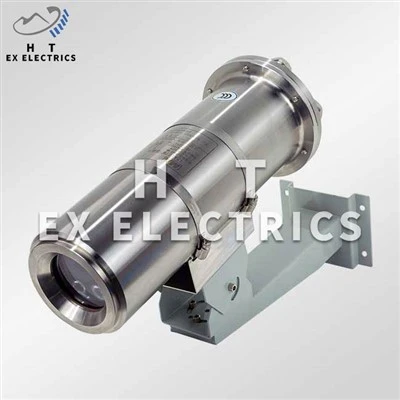

Technical Specifications & Parameter Matrix
|
Technical Parameter |
Model KBA127(A) (Explosion-Proof PTZ) |
Model KBA12H (Intrinsically Safe Infrared) |
|
Primary Protection Type |
Explosion-proof enclosure design |
Intrinsically safe electrical configuration |
|
Optical Transmission |
Single-mode fiber optic support |
Dual SC-type optical interfaces |
|
Network & Communication |
TCP/IP remote control protocol |
Ethernet optical signal output |
|
Rated Working Voltage |
Standard industrial DC / AC input options |
DC 12V rated input |
|
Imaging & Monitoring |
Remote pan, tilt, and zoom (PTZ) adjustment |
Integrated infrared low-light capture |
|
Application Suitability |
Long-distance roadway & zone monitoring |
Targeted underground operational points |
Why Partner with Us
Two Decades of Mining Specialization
Founded in 2003, our operations focus exclusively on electrical automation and explosion-proof safety equipment for underground coal mines, delivering engineering solutions aligned with rigorous hazard-area regulations.
Advanced Manufacturing Infrastructure
Production is supported by over 50 sets of advanced manufacturing machinery, including high-precision CNC lathes, machining centers, laser cutting systems, laser welding equipment, and automated welding robots.
Integrated Quality Assurance
Critical mechanical components and explosion-proof enclosures are machined and assembled in-house, ensuring strict dimensional tolerances, reliable sealing integrity, and consistent structural durability.
Typical Underground Applications

-
Conveyor Belt Monitoring
Supervise transfer chutes, belt alignment, and material flow to mitigate fire hazards and mechanical failures.
-
Equipment & Substation Rooms
Provide remote visual verification of unattended electrical substations, pumps, and ventilation equipment.
-
Underground Transport Routes
Monitor main haulage drifts, shaft stations, and traffic convergence points to enhance operational safety.
-
Centralized Surface Control Rooms
Link compatible optical cameras back to surface control terminals for continuous 24/7 observation and archival recording.
Manufacturing & Quality Assurance Standards
Reliable field performance relies on rigorous manufacturing and testing protocols:
Precision Machining & Enclosure Fabrication
Enclosures and mechanical components are produced using advanced CNC machining centers and automated cutting equipment to maintain strict dimensional tolerances for explosion-proof joints.
Structural Integrity & Welding
High-integrity welding processes and robotic assembly ensure structural durability against underground vibration and mechanical stress.
Factory Testing
Units undergo electrical safety testing, optical performance verification, and environmental simulation checks prior to dispatch.
Project Delivery & Logistics Coordination

Export-Grade Protective Packaging
Equipment is secured using moisture-resistant barriers, shock-absorbing foam inserts, and reinforced wooden crating designed to withstand long-distance maritime and land transit.

Customs and Compliance Documentation
Shipment packages include complete commercial invoices, packing lists, origin certificates, and technical test reports required for smooth customs clearance and site auditing.

Lead Time and Supply Tracking
Structured production scheduling ensures transparent delivery milestones, with regular progress updates provided from assembly to final port dispatch.
Frequently Asked Questions
As one of the most professional explosion-proof fiber optic camera manufacturers in China, we're featured by providing high quality products for mining communication system and mining automation equipment. Welcome to buy customized explosion-proof fiber optic camera from our factory.